Table of Contents
- Introduction
- What Are Screw Conveyor Systems?
- How Screw Conveyors Work
- Key Features of Screw Conveyor Systems
- Benefits of Using Screw Conveyors
- Technical Specifications
- Applications Across Industries
- Why Choose Custom Screw Conveyors?
- Maintenance Best Practices
- Frequently Asked Questions
- Conclusion
Introduction
Material handling plays a crucial role in modern industrial operations. Companies require efficient systems capable of transporting bulk materials while minimizing product loss and operational downtime.
Discover high-performance Systems designed for efficient material handling, smooth material flow, durability, and heavy-duty industrial applications across multiple industries.
Screw conveyor systems have become one of the most preferred material handling solutions due to their simple design, durability, and versatility. They provide controlled material movement and can be customized according to application-specific requirements.
Their ability to operate continuously while handling various material types makes them indispensable in many industrial sectors.
What Are Screw Conveyor Systems?
A screw conveyor is a mechanical material handling device that uses a rotating helical screw blade, commonly known as a flight, mounted on a central shaft to move materials along a trough or tube.
These conveyors are designed for transporting bulk materials horizontally, vertically, or at inclined angles depending on operational requirements.
They are commonly used in industries that require consistent and efficient movement of powders, granules, pellets, and semi-solid materials.
How Screw Conveyors Work
Material Feeding
Bulk material enters the conveyor through an inlet section.
Rotating Screw Mechanism
The rotating screw flight pushes the material forward through the conveyor casing.
Controlled Material Movement
Material moves at a controlled rate based on screw speed and conveyor design.
Material Discharge
The transported material exits through designated discharge points.
Key Features of Screw Conveyor Systems
High Strength and Durability
Manufactured using premium-grade materials to withstand demanding industrial environments.
Custom Built to Requirements
Available in various sizes, diameters, lengths, and configurations.
Smooth and Efficient Material Flow
Provides continuous and controlled transportation of bulk materials.
Heavy-Duty Industrial Construction
Designed for high-capacity and long-term industrial operation.
Precision Engineering
Fabricated with strict quality standards for reliable performance.
Low Maintenance Requirements
Simple mechanical design reduces maintenance needs and operational costs.
Benefits of Using Screw Conveyor Systems
| Benefit | Description |
|---|---|
| Efficient Material Transfer | Ensures smooth and continuous movement |
| Reduced Manual Handling | Improves workplace productivity |
| Space-Saving Design | Requires minimal installation space |
| Customizable Configuration | Suitable for diverse applications |
| Reliable Operation | Supports continuous industrial processes |
| Cost-Effective Solution | Low operational and maintenance costs |
| Enhanced Safety | Minimizes material spillage |
| Long Service Life | Built for durability and performance |
Technical Specifications
| Specification | Details |
|---|---|
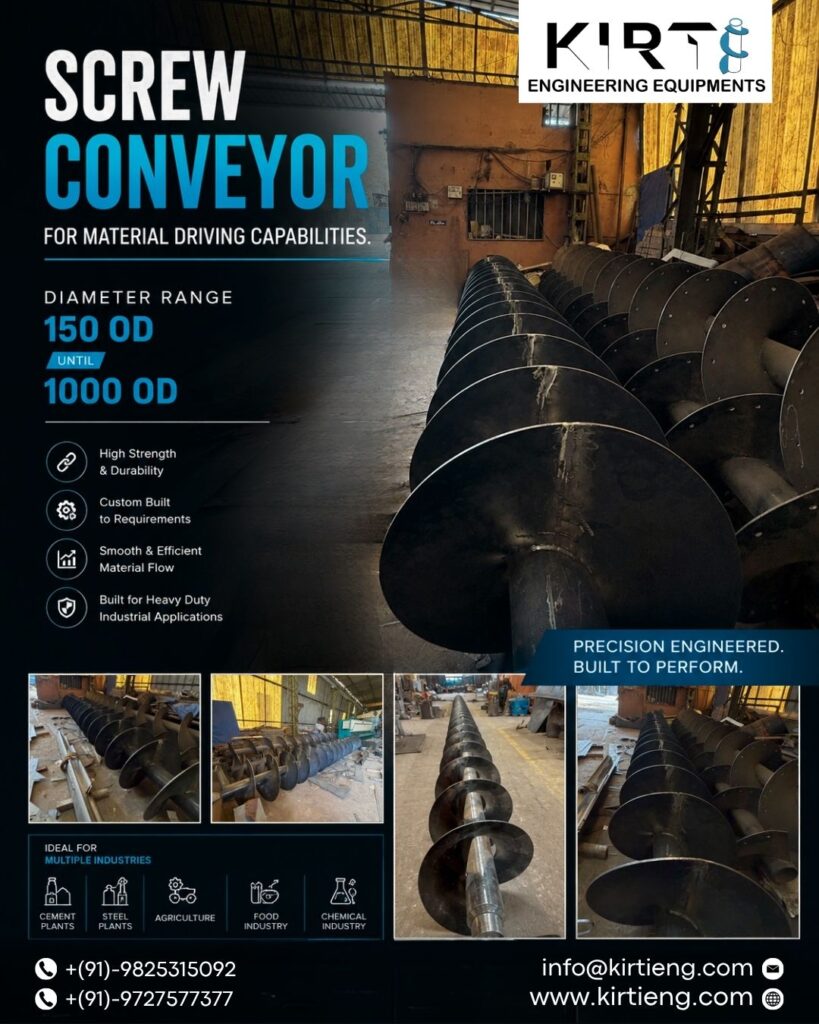
| Diameter Range | 150 OD to 1000 OD |
| Material Construction | Mild Steel, Stainless Steel, Alloy Steel |
| Conveyor Type | Horizontal, Inclined, Vertical |
| Application | Bulk Material Handling |
| Capacity | Customizable |
| Surface Finish | As Required |
| Design | Heavy Duty Industrial |
| Customization | Available |
Applications Across Industries
Cement Plants
Efficiently transports cement, clinker, fly ash, and related materials.
Steel Plants
Used for handling raw materials, scrap, and industrial by-products.
Agriculture Industry
Supports movement of grains, seeds, fertilizers, and feed materials.
Food Processing Industry
Handles powders, ingredients, and food-grade materials.
Chemical Industry
Provides controlled transfer of chemicals and industrial compounds.
Manufacturing Facilities
Facilitates movement of raw materials and production inputs.
Why Choose Custom Screw Conveyors?
Every industry has unique material handling requirements. Custom screw conveyor systems allow businesses to optimize efficiency by selecting the appropriate diameter, pitch, length, material construction, and operating configuration.
Customized systems offer:
- Better material flow control
- Improved operational efficiency
- Reduced maintenance costs
- Enhanced process integration
- Greater flexibility for future expansion
Maintenance Best Practices
Regular Inspection
Monitor screw flights, bearings, and drive components.
Lubrication
Maintain proper lubrication schedules for moving parts.
Material Flow Monitoring
Prevent overloading and material buildup.
Periodic Cleaning
Remove accumulated materials to maintain efficiency.
Component Replacement
Replace worn parts promptly to avoid downtime.
Frequently Asked Questions (FAQs)
What is a screw conveyor system?
A conveyor system is a mechanical device used for transporting bulk materials through a rotating screw mechanism.
What materials can screw conveyors handle?
They can handle powders, granules, cement, chemicals, grains, food products, and various bulk materials.
Are screw conveyors customizable?
Yes. Screw conveyors can be customized based on diameter, length, material type, and application requirements.
Which industries use screw conveyors?
Cement, steel, agriculture, food processing, chemical, and manufacturing industries commonly use screw conveyors.
What is the typical diameter range of industrial screw conveyors?
Industrial screw conveyors are available in various sizes, including diameters ranging from 150 OD to 1000 OD.
Are screw conveyors suitable for heavy-duty applications?
Yes. Heavy-duty screw conveyors are specifically designed for demanding industrial environments and continuous operation.
Conclusion
Screw conveyor systems are among the most effective solutions for bulk material handling across industrial sectors. Their ability to provide smooth material flow, durability, and operational efficiency makes them an essential component in modern manufacturing and processing facilities.
Kirti Engineering Equipments manufactures precision-engineered systems designed to meet the specific needs of diverse industries. With customizable designs, robust construction, and reliable performance, these conveyors help businesses improve productivity while ensuring efficient material handling operations.
Check this :- https://heavyindustries.gov.in/